Achieving precise color reproduction is challenging on any medium, but synthetic textiles present unique hurdles. Whether producing dye-sublimated soft signage, trade show exhibits, activewear, or commercial upholstery, printing on synthetic fibers like polyester, nylon, and elastane differs fundamentally from printing on paper or vinyl.
Color on fabric is dynamic. It shifts with yarn weave, interacts with ambient light, and changes under heat and pressure.
Too often, teams approve artwork on a monitor or paper proof, only to find that finished polyester banners look dull, corporate blues lean purple, or display panels clash under showroom lights. Resolving these issues requires understanding synthetic polymer physics, optics, and disciplined proofing. Here are five mistakes to avoid when color matching synthetic fabrics—and how to get consistent results every time.
1. Evaluating Colors Under Uncontrolled Lighting (The Metamerism Trap)
The quick answer: Approving fabric colors under standard office lighting leads to metameric failure, where two colors match under one light source but clash under another.
A common pitfall in textile printing is metamerism in synthetic textiles. Metamerism occurs when two swatches match under one light spectrum (like daylight) but diverge sharply under retail LEDs, cool fluorescents, or halogen bulbs.
Synthetic fibers like polyester and nylon possess crystalline structures that scatter light differently than paper or natural fibers. When dyes bond with synthetic polymers, their spectral reflectance curve changes uniquely.
Common Mistake to Avoid: Never inspect swatches under random desk lamps or hallway lights.
Always evaluate fabric matches inside a standardized light booth. View samples under at least three illuminants: D65 (daylight), commercial store fluorescents (CWF/TL84), and Illuminant A (incandescent). If the finished piece is bound for a trade show or retail space, evaluate the strike-off under that venue’s specific lighting.
2. Neglecting Cross-Substrate Reflectance Across Multi-Material Displays
The quick answer: Applying identical CMYK or RGB values across both rigid and fabric substrates creates visible color discrepancies due to differences in surface sheen and light absorption.
In visual merchandising and event design, synthetic fabric graphics rarely exist in isolation. A branded fabric backdrop often stands directly alongside hanging signs, point-of-purchase displays, or rigid perimeter panels.
A frequent error is assuming that sending the same Pantone code to different printers yields identical results across materials. A matte woven polyester absorbs light and diffuses it across yarn filaments. By contrast, a flat UV-printed rigid foam board features a dense, smooth surface with high specular reflection. Even with calibrated ink formulations, the human eye perceives the fabric as darker and more saturated than the rigid panel.
Harmonizing mixed-media installations requires cross-profiling. Technicians must adjust ink saturation curves and tone values for the textile’s optical properties rather than forcing a single file onto both rigid and soft substrates.
3. Ignoring Thermochromism and Heat-Press Dwell Times
The quick answer: Heat-activated disperse dyes undergo thermochromic shifts during sublimation, meaning colors appear darker when warm and change as the fabric cools and rehydrates.
In synthetic printing, dye sublimation color management requires strict thermal discipline. Disperse dyes do not simply coat fabric; heat and pressure vaporize dye into gas while opening polyester polymer pores. When cooled, the polymer locks the dye inside the fiber.
This process introduces two critical variables:
- Thermochromism: Freshly pressed synthetic fabric does not display its true hue while warm. As polyester cools and reabsorbs ambient moisture over 20 to 30 minutes, color stabilizes. Measuring warm prints with a spectrophotometer produces false readings.
- Calendar Dwell-Time Shifts: A temperature swing of 5°F or slight speed differences on a heat calender alters dye activation. Insufficient heat leaves dyes partially converted, while excessive heat scorches optical brighteners, shifting whites toward gray.
4. Relying on Paper Swatches Instead of Fabric Strike-Offs
The quick answer: Paper proofs cannot simulate ink diffusion, fiber translucency, or yarn absorption; testing colors directly on production-grade synthetic fabric is non-negotiable.
Designers often rely on paper proofs or Pantone formula guides when approving colors. While formula guides are helpful communication baselines, relying on paper to predict fabric performance leads to costly reprints.
Paper is opaque, rigid, and uniform. Synthetic fabrics vary widely—ranging from dense backlit knits to sheer mesh and stretch spandex. Inks penetrate between yarn bundles, creating internal reflections that alter perceived depth and chromatic intensity.
Implementing a strict textile strike-off approval process prevents run errors. Always produce a physical strike-off on the actual production fabric roll using scheduled printers, ink sets, and calendar settings. A small test print saves thousands in wasted inventory.
5. Disregarding Fiber Weave, Yarn Sheen, and Fabric Stretch
The quick answer: Fabric construction alters visual perception; identical dye densities read substantially differently on matte, satin, knit, or tensioned stretch textiles.
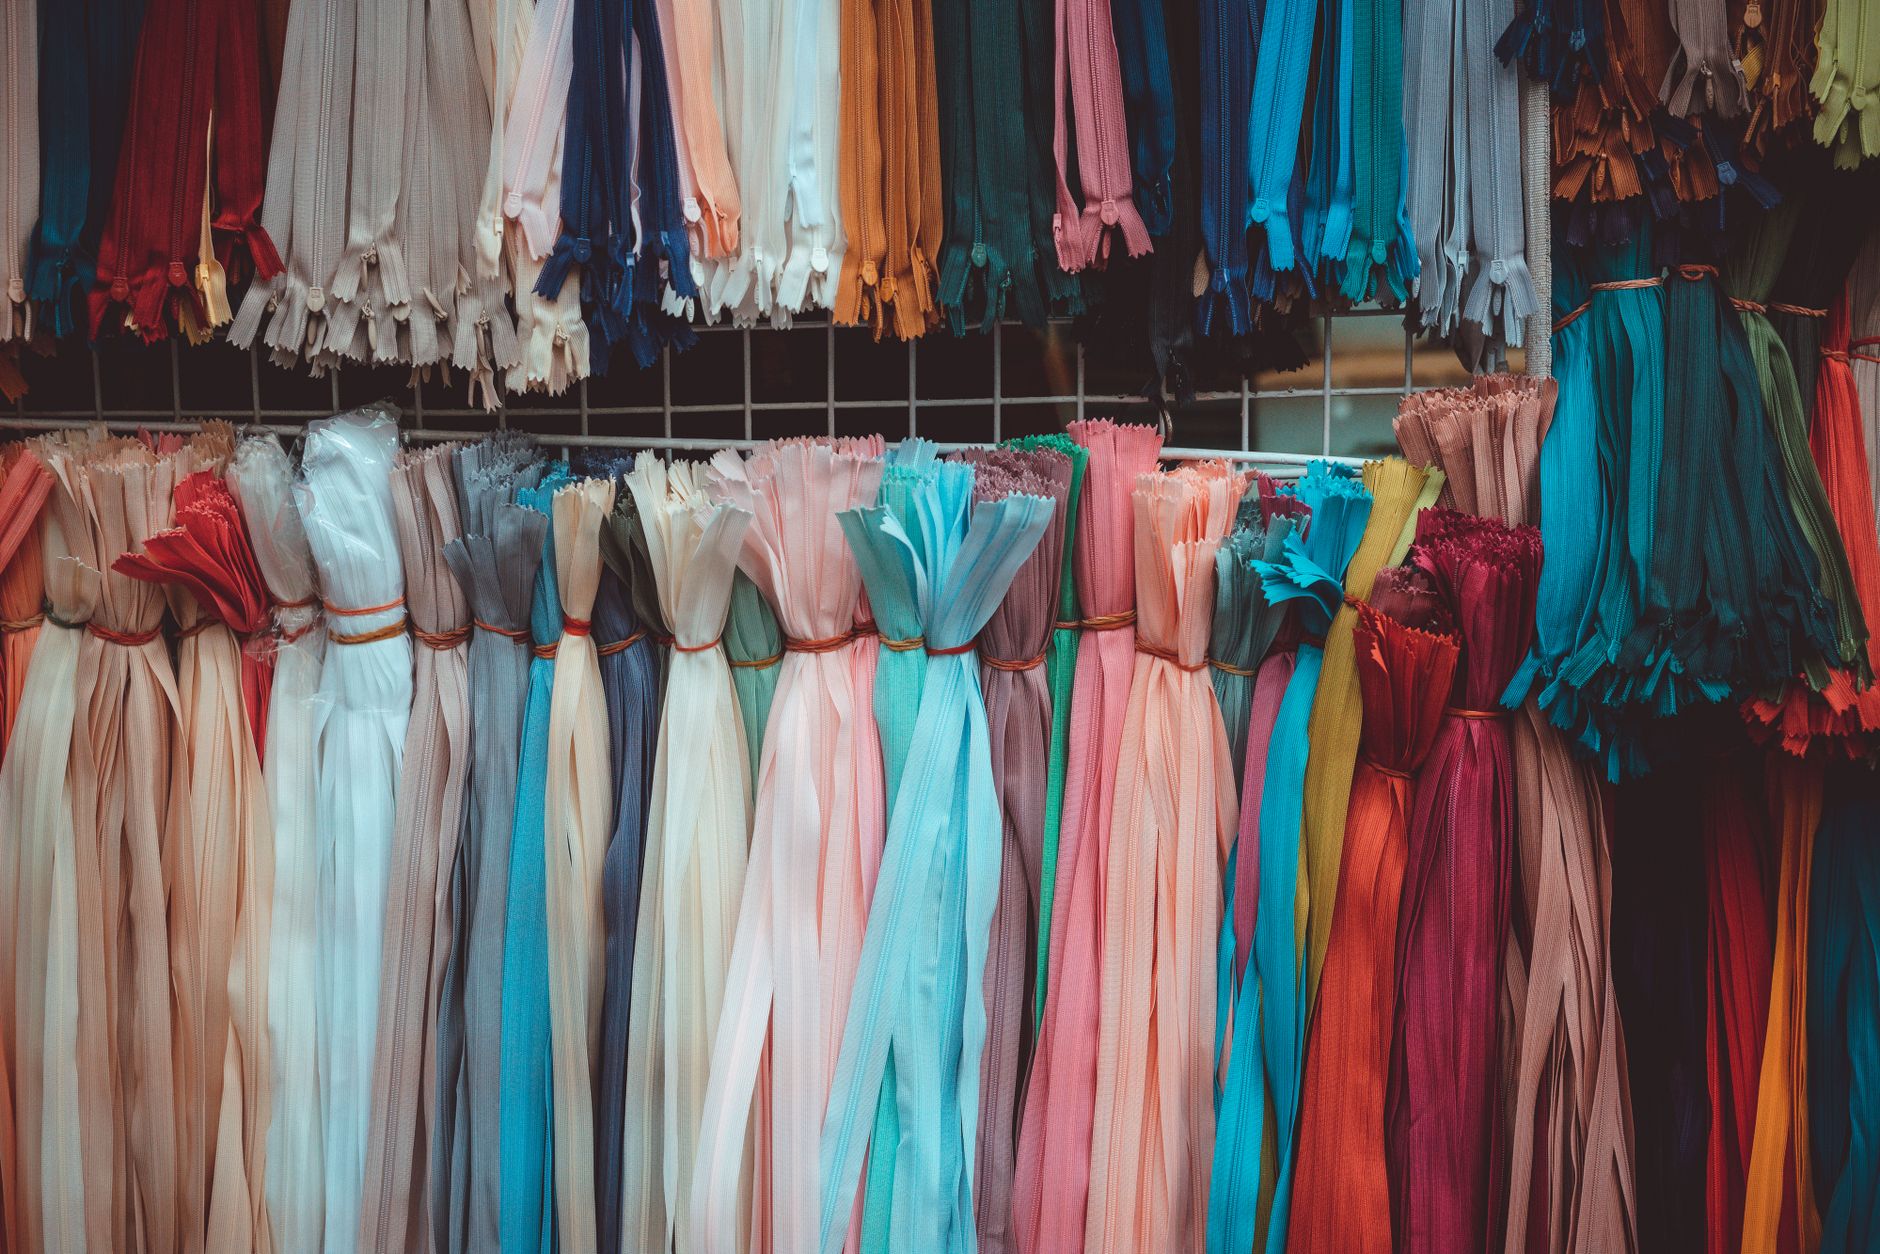
Synthetic fabrics come in diverse textures and finishes. A smooth polyester satin reflects light directionally to produce intense highlights, while open-hole mesh lets light pass through, desaturating artwork.
Consider these factors during color formulation:
- Yarn Luster: Trilobal polyester fibers reflect light with a silky sheen that brightens hues, whereas round staple fibers create a subdued, matte appearance.
- Elastic Tension: Tension fabrics containing elastane stretch when installed on aluminum frames. Stretching widens knit gaps, diluting dye density and making deep blacks look washed out.
- Backlighting and Opacity: Frontlit fabrics require standard ink limits, whereas backlit silicone edge graphics (SEG) need double-density ink to prevent washed-out tones when lit from behind.
Color matching synthetic fabrics requires chemistry, optical physics, and process discipline. Because synthetic fibers interact dynamically with heat, dye chemistry, and ambient light, consistency demands looking beyond traditional print assumptions. By controlling viewing illuminants, accounting for substrate differences, respecting sublimation thermal cycles, and demanding physical strike-offs, print professionals eliminate guesswork and deliver stunning, color-accurate textiles on every run.